If you’ve ever worked with metal components that need to hold up under high stress, wear, or extreme temperatures, you know induction quenching and tempering lines are the workhorses that make that happen. As a supplier who’s spent 15 years designing, building, and installing these lines for automotive parts manufacturers, farm equipment makers, and heavy machinery producers, I can’t tell you how many times I’ve gotten a call from a plant manager panicking because their new line won’t fit their existing space—or worse, their site’s hidden issues will make the line fail within a month of startup. Induction Quenching and Tempering Production Line
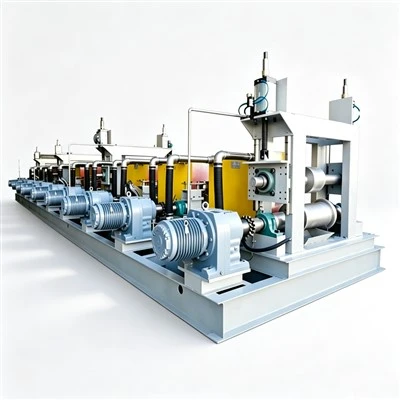
Induction quenching and tempering isn’t just plug-and-play equipment. The site it lives on directly impacts uptime, part quality, energy bills, and even worker safety. Over the years, I’ve walked into sites that look perfect on blueprints but have a 10-foot drop-off 2 feet from where the line is supposed to go, or a 200-amp circuit that can’t handle the line’s 500-peak kilowatt load. Today, I’m breaking down exactly what you need to plan for before your line arrives—no jargon, just real-world lessons I’ve learned from years of on-site installs.
First and foremost, let’s talk about physical space, and I’m not just talking about the dimensions on your CAD drawing. A common mistake I see is plant managers only measuring the footprint of the line itself. But induction lines need access for every step of the process: unloading raw parts, moving them through the induction coil, quenching, tempering, inspection, and then loading finished parts. Let’s get specific here. A standard continuous induction line for automotive crankshafts, for example, is roughly 80 feet long and 12 feet wide, but you need at least 3 feet of clearance on every side for maintenance, part transfer systems, and safety guards. If you have to squeeze the line into a space where a forklift can’t maneuver with raw parts, you’re looking at hours of downtime every week, not to mention increased risk of part damage from rough handling.
Then there’s the floor itself. This is a detail that gets overlooked all the time. Induction lines are heavy—we’re talking 15,000 to 30,000 pounds for a mid-sized line, and up to 50,000 pounds for large lines processing heavy equipment axles. So the floor’s load-bearing capacity is non-negotiable. When we site a new line, we require a minimum of 2,000 pounds per square foot of uniform capacity, and we test the floor with a heavy forklift or weighted skid before even delivering the equipment. We once had a customer who had a 1,500-pound-per-square-foot floor that passed their plant’s general inspection but cracked 3 inches under the line’s main power cabinet during installation. We had to bring in concrete contractors to pour a reinforced pad that weekend, delaying their startup by 3 days and costing them thousands in lost production. That’s a $10,000 mistake they’d rather avoid.
It’s not just weight on the floor—vibration resistance matters too. Induction heating uses high-frequency electromagnetic currents, but the line’s own moving parts (conveyors, quenching pumps, tempering furnaces) generate constant vibration that can throw off part alignment if the floor isn’t stable. If your plant is near a press line, a large conveyor, or any other heavy machinery that runs 24/7, that vibration can accumulate over time, leading to uneven quenching (which means parts fail hardness tests) and broken conveyor chains. We recommend a separate reinforced concrete slab for the induction line, isolated from other equipment, or at minimum, a floor that’s been professionally engineered to minimize vibration. A few years back, a farm equipment manufacturer tried skipping this for a line processing plow blades. Within 6 months, their part hardness variation hit 15%, well below the 5% required for their parts, because vibration was shifting the position of the induction coil. They had to tear out part of their plant to add a vibration pad—total cost of over $50,000.
Next up is power, and this is another area where generic plant electrical systems almost never cut it. Induction quenching lines draw massive amounts of power, and they’re not linear loads—they spike and dip as the line cycles through heating, quenching, and tempering. A standard line will have a peak power demand of anywhere from 200 kW to 1,200 kW, and you need a dedicated power transformer, separate from the rest of your plant. Why? Because if you run the line off a shared circuit, starting it will dim lights, crash your PLC systems, and even cause other machinery to shut down, leading to unplanned downtime. We also require consistent voltage within 5% of the line’s rated voltage. A voltage drop of even 10% can reduce the induction coil’s heating efficiency by 20%, meaning you’re using way more energy to get the same heat, and parts won’t reach the required hardness.
We always work with the customer’s electrical team to do a power study before installation. That study tells us if they have enough incoming power capacity, if the transformer size is correct, and if their wiring can handle the amperage. Last year, a small job shop called us in a panic because they wanted a line for fastener heat treatment. Their plant’s main transformer was rated at 300 kW, and their line needed 450 kW. Instead of upgrading the transformer, they tried to tap into a sub-circuit, and when they fired the line up, it tripped every breaker on the floor. We had to arrange for an emergency transformer upgrade for them, which added $8,000 to their project. It’s way cheaper to do the power study upfront than fix that kind of mistake.
Cooling is the unsung hero of induction lines, and it’s also the thing that causes the most call-outs after startup. When you heat a metal part to 1,700 degrees Fahrenheit and then quench it with water, and run a tempering furnace at 500 degrees for hours, you need a reliable cooling system to keep everything from overheating. Most induction lines use closed-loop cooling systems, not tap water, because tap water has minerals that will clog coils and pumps over time. We require a cooling system that can deliver at least 10 gallons per minute per 100 kW of line power, with a maximum water temperature of 80 degrees Fahrenheit. If your cooling water is hotter than that, your quenching process is less effective, and you’ll have inconsistent part quality.
I can’t tell you how many times I’ve had to troubleshoot a line where the cooling tower was too small for the line’s power. A customer in Detroit once had a line for brake rotors that kept overheating the induction coil during night shifts, when their plant’s cooling demand was highest. They had a cooling tower rated for their general plant load, not the line’s peak cooling needs. We ended up adding a smaller auxiliary cooling unit just for the line, which solved the problem, but it delayed their production run by two weeks. If they’d checked the cooling requirements before ordering the line, that wouldn’t have happened. Also, make sure your cooling system has backup capacity—if the tower goes down for an hour, you need a way to keep the line from overheating while you fix it. A simple backup pump and a buffer tank are non-negotiable here.
Then there’s air, both compressed and ambient. Induction lines use compressed air for a lot of things: blowing water off parts after quenching, clearing debris from the conveyor, and cooling small components. We recommend a dedicated compressed air line for the line, separate from other plant tools, with a pressure of 90 to 110 PSI. If the air pressure drops, parts won’t dry properly, leading to rust during storage, or debris will get left on the line, causing part damage. Ambient air quality matters too, especially for tempering. If your plant is in a dusty environment—like a foundry or a lumber mill—you need to have filtered air going into the tempering chamber. Dust can build up on the parts during tempering, leaving a layer of grime that has to be removed before painting or assembly. We always add air filtration systems for lines in harsh environments, and it’s a small cost upfront that saves a lot of rework later.
Finally, safety and regulatory compliance, which are non-negotiable no matter what kind of site you have. Induction lines work with high voltage, high temperatures, and moving parts, so they have to meet OSHA standards, EU machinery directives (for international customers), and any local environmental regulations. For example, induction quenching can produce metal fumes from small parts, so you need a proper exhaust system that vents those fumes outside, not into the plant. We always work with customers to design an exhaust system that meets their local air quality rules, because failing an inspection after startup can shut down your entire operation.
Safety guards are another big one. The line has to be enclosed with light curtains or safety gates that shut down the line if someone reaches into the moving parts or the hot zones. I once had a customer who tried to save money by skipping the light curtains, and their operator got their hand caught in the conveyor during a test run. It was a preventable mistake, and it cost them hundreds of thousands in workers’ comp and lost production. Don’t cut corners here.
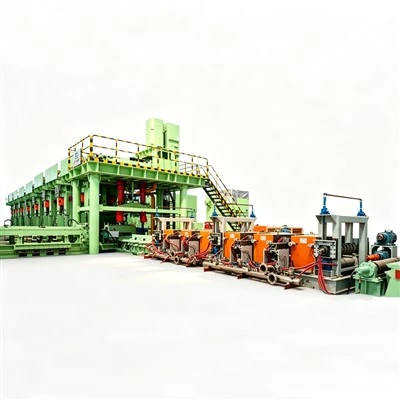
At the end of the day, installing an induction quenching and tempering line isn’t just about getting the right equipment—it’s about getting the right site that supports that equipment. As a supplier, my number one goal isn’t just to sell you a line—it’s to make sure it runs smoothly for years, so you can hit your production targets and make parts that last. If you’re planning to add an induction line to your operation and want to walk through your site, get a power study, or answer any questions about installation requirements, reach out to our team to set up a consultation. We’ll come to your plant, do a full assessment, and give you a clear plan that avoids the costly mistakes I’ve seen too many customers make.
Steel Billet Reheating Furnace References
ASM International. (2019). Induction Heating and Heat Treating. Materials Park, OH: ASM International.
Occupational Safety and Health Administration (OSHA). (2022). Machine Guarding Requirements for Hot Process Equipment. Washington, D.C.: U.S. Department of Labor.
International Organization for Standardization (ISO). (2021). ISO 9001:2015, Quality Management Systems – Requirements. Geneva, Switzerland: ISO.
National Fire Protection Association (NFPA). (2020). NFPA 70: National Electrical Code. Quincy, MA: NFPA.
Hebei Yuantuo Electromechanical Equipment Manufacturing Co., Ltd.
As one of the most professional manufacturers and suppliers of induction quenching and tempering production line in China, our products have good reputation in the market. Please rest assured to buy advanced equipment made in China here and get quotation from our factory. Customized orders are welcome.
Address: Yanshan Street West and Jialingjiang Road North, Economic and Technological Development Zone, Wuqiao County, Cangzhou City, Hebei Province, China
E-mail: yuantuotech01@gmail.com
WebSite: https://www.yuantuoem.com/
