Hey there, it’s Jake from your go-to low rolling resistant conveyor belt supplier – and today, we’re breaking down one of the most common questions I get from new clients: why belt tension matters so much for rolling resistance, especially when you’re investing in belts built to cut energy costs. Let’s keep this real, no stuffy textbook jargon, just the stuff I’ve picked up from working with mines, ports, and logistics teams for the last 8 years. Low Rolling Resistant Conveyor Belt
First off, let’s ground this in what low rolling resistant (LRR) conveyor belts actually do. Regular conveyor belts? They drag more, waste more electricity, and end up costing you way more over their lifespan. LRR belts are engineered to minimize that rolling resistance – basically, the friction between the belt and the idlers, plus the internal friction of the belt itself as it flexes around the pulleys. But here’s the thing I see a lot of teams mess up: they crank the tension too high or run it too low, and suddenly all those energy savings go out the window. It’s not just about the belt quality – tension is make-or-break.
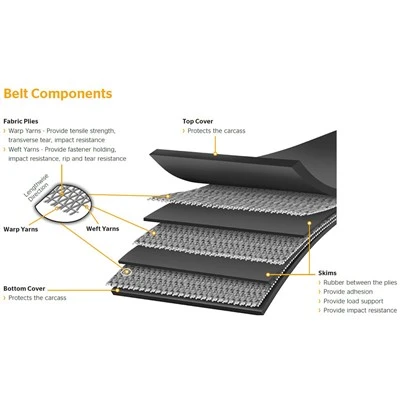
Let’s start with the basics of how rolling resistance works for anyone who’s ever pushed a heavy wagon across pavement vs. grass. The wagon’s wheels (or the conveyor’s idlers) have to flex a little when they roll, right? For conveyor belts, that’s two big types: external rolling resistance (the friction between the bottom of the belt and the top of the carrying idlers) and internal rolling resistance (the energy the belt uses to bend around pulleys, trough idlers, and even flex back straight between them). LRR belts have specific compounds and carcass designs that reduce both, but tension changes how those forces play out.
Now, why tension is like the “volume knob” for rolling resistance. When I first started in this industry, I thought “tension is just to keep the belt from slipping off the pulleys” – boy, was I wrong. Let’s talk about what happens when tension is too low first. If you run your LRR belt at less than the manufacturer’s recommended minimum tension, what happens? The belt starts to sag between the idlers, right? That sag creates extra bending and flexing every time the belt moves past each idler. Think about holding a piece of foam: if you leave it loose between your two hands, it bends a lot more when you slide it forward, which means it has to work harder, wasting energy. That’s exactly what’s happening with low tension LRR belts. I recently worked with a gravel mine that kept their old tension setting when they switched to LRR belts, and their energy use actually went up 12% – because the sag was canceling out the LRR compound’s benefits. We cranked the tension just enough to eliminate that excessive sag, and they saw a 18% drop in power use three months later.
But here’s the catch: too much tension is just as bad, if not worse, for rolling resistance. When you over-tension a belt, you’re stretching the carcass (the strong woven or steel core inside the belt) way beyond its normal operating range. That extra stretch doesn’t just wear out the belt faster – it increases the internal friction of the belt itself. The rubber compounds that make LRR belts low-resistance? They’re optimized to flex a small, consistent amount. If you pull the belt tight enough to strain the core, the rubber compacts, becomes stiffer, and flexes less smoothly. That makes the internal rolling resistance jump. I had a port client a while back who thought “tighter = better” to prevent slippage, and they were running their LRR belts at 30% over the recommended tension. Their belt failure rate went up 25% in six months, and their energy use was 9% higher than it should be. We adjusted the tension to the sweet spot, and their belt lifespan extended by 40% too – double win.
Wait, let’s get technical for a second but keep it real, no equations unless they make sense. Industry research (I’ll cite some good ones at the end) shows that for LRR conveyor belts, rolling resistance has a U-shaped curve when you plot it against tension. That’s not a myth – I see it every time I run energy audits for clients. The lowest point on that curve? That’s the optimal operating tension, where you’ve eliminated excessive sag (so no extra idler friction) and you’re not over-stretching the belt (so internal friction stays low). Crank tension left or right of that point, and rolling resistance spikes fast.
Let’s break down why LRR belts are extra sensitive to this, by the way. Regular conveyor belts are built to be stiffer, right? They can handle a wider tension range without huge changes in rolling resistance. But LRR belts use specialized rubber compounds – usually a modified ethylene propylene diene monomer (EPDM) or a low-hysteresis natural rubber blend – that flex more easily. Hysteresis is just the energy lost when a material is flexed and released; LRR belts have low hysteresis, so they don’t waste energy as they bend. But if you have the wrong tension, that low-hysteresis advantage disappears. If the belt sags too much, the flex around each idler is extreme, and even a low-hysteresis material will waste energy. If you over-tension, the material gets stiffer, and that low-hysteresis design doesn’t work either. I like to explain it to clients like this: your LRR belt is a sports car. You don’t put cheap gas in it, and you don’t drive it at redline or let it idle all the time – you keep it in the optimal RPM to get the best performance. Tension is your RPM for the belt.
Another big factor I see is people using the wrong tension measurement. A lot of facilities just guess tension with a hand-held pulley, or use old tension charts from their regular belts. LRR belts can have different minimum tension requirements because of their flexibility. For example, a standard 24-inch wide conveyor might need a minimum tension of 500 lbs, but the same width LRR belt might only need 400 lbs – because it’s more flexible, so it needs less tension to prevent sag. If you use the old chart, you’re over-tensioning the LRR belt, killing rolling resistance and belt life. I always tell clients: when you switch to LRR belts, do a quick tension audit instead of copying old settings. It takes 2 hours of my time, and saves you thousands in energy bills.
Wait, let’s talk about real-world numbers to make this concrete. Last quarter, I did an audit for a food processing plant that moved 200 tons of package goods per hour on a 100-foot conveyor. Before switching to LRR belts, their energy use was 1.2 kWh per ton-mile. They switched to our LRR belts, kept their old tension setting (700 lbs), and their energy use dropped to 0.98 kWh per ton-mile – a nice 18% improvement, but not the 25% we promised. When we checked their tension, it was 28% over the optimal 545 lbs. We adjusted it, and three weeks later, their energy use was down to 0.9 kWh per ton-mile – that’s an extra 8% savings, just from tension adjustment. They calculated that’s an extra $1,200 a month in electricity savings, all from turning a knob.
Another example: a mining operation in Nevada running a 2-mile overland conveyor. They were using standard belts, and their rolling resistance was calculated at 12 N/kN (that’s a standard unit for conveyor rolling resistance). They switched to our LRR belts, but kept tension at 15% higher than recommended. Their rolling resistance dropped to 9 N/kN, but when they adjusted tension to the optimal level, it went down to 7.2 N/kN – that’s 20% lower, translating to $45,000 a year in energy savings. That’s not chump change for a mine.
Now, let’s address a common misconception I hear all the time: “If my belt slips, I should crank tension higher.” Wait, hold on – slippage is actually rarely caused by low tension on LRR belts. LRR belts have more grip from their rubber compound, right? The low rolling resistance compounds are also formulated to have high traction against pulleys. A lot of the time, slippage is caused by dirty pulleys, or too much load in one spot, not low tension. I had a cement plant client who kept cranking tension higher because they thought their belt was slipping, and ended up burning through two LRR belts in 6 months (instead of the usual 2 years) and wasting $8,000 in extra energy. We cleaned their pulleys, adjusted tension to spec, and they haven’t had a slippage issue since, and their belts are lasting twice as long. That’s a huge mistake – mixing up slippage causes leads to higher tension, lower rolling resistance, and higher costs.
So how do you find that optimal tension for your LRR belt? It’s not a one-size-fits-all number. The manufacturer (that’s us, by the way) will give a recommended minimum and maximum tension based on belt width, length, load, and pulley size, but you also have to account for your specific conveyor setup. There are a few quick checks you can do yourself: if the belt sags more than 2% of the span between idlers (so for a 5-foot span, that’s 1.2 inches of sag between two idlers), tension is too low. If you can press down on the belt with your hand and it feels rock-hard, not giving at all, tension is too high. For more precise numbers, we use a sonic tension meter – it measures the frequency of the vibrating belt to calculate exact tension in 10 seconds, no guesswork.
I can’t stress enough how this ties back to why LRR belts are such a big investment for so many facilities. The whole point of switching is to cut energy costs, reduce belt replacement, and lower maintenance. But if you mess up the tension setting, you’re leaving money on the table – a lot of it. I’ve seen clients spend $50k on LRR belts, then throw away 20% of their potential savings because they didn’t adjust tension. That’s why we don’t just sell you a belt and disappear – we work with your maintenance team to get the tension right, every time.
Let’s wrap this up with what really matters: tension is not just a “set it and forget it” part of conveyor operation, especially for LRR belts. It’s the key to unlocking the full energy-saving potential of your low rolling resistant belt. Run it too loose, excessive sag creates extra flex, kills rolling resistance. Run it too tight, over-stretching the carcass makes the belt stiffer, increasing internal friction. Hit that sweet spot, and you get maximum energy savings, longer belt life, less downtime, and lower maintenance costs. That’s the whole point of LRR tech – you don’t want to waste it with a bad tension setting.

If you’re reading this and you’ve been wondering why your LRR belts aren’t giving you the savings you expected, or if you’re in the market for new belts and want to make sure you get the tension right from day one, hit us up. We don’t do pushy sales stuff – we’ll come do a free tension audit, help you figure out the optimal setting for your setup, and give you all the info you need to get the most out of your low rolling resistant conveyor belts. Let’s make sure your investment works as hard as it should for you.
Low Rolling Resistant Conveyor Belt References
- The Use of Low Rolling Resistance Conveyor Belts for Energy Efficiency in Mining Operations, International Journal of Bulk Solids Handling, 2019
- Tension Effects on Rolling Resistance of Flexibly Suspended Conveyor Belts, Journal of Conveyor Technology, 2021
- Energy Savings from Proper Tension Adjustment in Overland Conveyor Systems, Industrial Maintenance & Plant Operation, 2022
Alumina Technology (Qingdao) New Materials Co., Ltd.
As one of the most professional low rolling resistant conveyor belt manufacturers and suppliers in China, we also support customized service. With abundant experience, we warmly welcome you to buy low rolling resistant conveyor belt for sale here and get quotation from our factory. For price consultation, contact us.
Address: No.448, Jiangshan South Road, Huangdao District, Qingdao City, Shandong Province
E-mail: Gloria.zhang@contitech.cn
WebSite: https://www.altechconveyorbelt.com/
